


3D suppressors (Page 9 of 11)

|
Originally Posted By Blob: If you mean 0.2mm, not recommended. I use 0.6mm with filled material to avoid clogs. A small nozzle will clog instantly and give a slightly weaker print in addition to taking longer. Originally Posted By Blob: Originally Posted By Network_Daddy: The one I saw was printed with a 2mm nozzle. Is that necessary or just making it take more time for no benefit? If you mean 0.2mm, not recommended. I use 0.6mm with filled material to avoid clogs. A small nozzle will clog instantly and give a slightly weaker print in addition to taking longer. This print was super clean but didn’t know about strength. |
|
Originally Posted By DFARM: I have a spool of sunlu pa6-cf coming from Amazon. I was planning on getting an amsHT at some point but is it not good enough for the pa6-cf? If it's marginal, can I run the spool in my shop air fryer for 12-24 hours at 212f(100c) and then print it from the amsHT? Also, does anyone know if I'll be able to print it from the aux nozzle on my x2d, or will I need one of the multi-ams hubs and use the main nozzle? It might be a bit ghetto but I use the middle sized Vevor fruit dehydrator with a Bowden tube quick connect screwed into a hole I drilled the back to run the filament through. They max out at 195* and have a 24hr timer. I cut slits into a piece of 3/4 copper that slides over the racks that will hold 3 1kg rolls. It has weeks of straight run time and is still cranking, cost like 100 bucks and works like a champ. |
|
Originally Posted By CFletch: The markings were not covered under SS v ATF (the one you get covered by as a GOA member), but are covered under Jensen v ATF (donate $10 to FPCAF to be covered) Originally Posted By CFletch: Originally Posted By scul: Originally Posted By DFARM: Silly question that maybe someone in this thread has some ideas about. Are you guys worried about marking requirements? It looks to me like there might still be a need to mark home built cans because I believe there are non-tax related laws that require it Yea, the marking requirements were not enjoined, so I'm pretty sure you still have to mark them. I also assume you cannot use a Trust, unless the trust is somehow a member of GOA or another specified group. @CFletch @DFARM Looking at this more, and I'm pretty sure the marking requirements are still intact. Marking is required per 5842(a), and only 5842(b) and 5861(i) were enjoined by Jensen. As I read it, you can possess an unmarked can, but if you make it, the markings need to be applied CFletch, if you have further clarification on this, it would be much appreciated. I'd genuinely love to be shown that this reading is wrong. https://saf.org/wp-content/uploads/2026/08/TX-NFA-opinion.pdf (Last page) The Jensen plaintiffs are entitled to relief from two additional NFA provisions that only they challenge. See supra, n.10; 26 U.S.C. §§ 5842(b), 5861(i). https://www.law.cornell.edu/uscode/text/26/5842 26 U.S. Code § 5842 - Identification of firearms (a) Identification of firearms other than destructive devices Each manufacturer and importer and anyone making a firearm shall identify each firearm, other than a destructive device, manufactured, imported, or made by a serial number which may not be readily removed, obliterated, or altered, the name of the manufacturer, importer, or maker, and such other identification as the Secretary may by regulations prescribe. (b) Firearms without serial number Any person who possesses a firearm, other than a destructive device, which does not bear the serial number and other information required by subsection (a) of this section shall identify the firearm with a serial number assigned by the Secretary and any other information the Secretary may by regulations prescribe. (c) Identification of destructive device Any firearm classified as a destructive device shall be identified in such manner as the Secretary may by regulations prescribe. https://www.law.cornell.edu/uscode/text/26/5861 26 U.S. Code § 5861 - Prohibited acts It shall be unlawful for any person— (a) to engage in business as a manufacturer or importer of, or dealer in, firearms without having paid the special (occupational) tax required by section 5801 for his business or having registered as required by section 5802; or (b) to receive or possess a firearm transferred to him in violation of the provisions of this chapter; or (c) to receive or possess a firearm made in violation of the provisions of this chapter; or (d) to receive or possess a firearm which is not registered to him in the National Firearms Registration and Transfer Record; or (e) to transfer a firearm in violation of the provisions of this chapter; or (f) to make a firearm in violation of the provisions of this chapter; or (g) to obliterate, remove, change, or alter the serial number or other identification of a firearm required by this chapter; or (h) to receive or possess a firearm having the serial number or other identification required by this chapter obliterated, removed, changed, or altered; or (i) to receive or possess a firearm which is not identified by a serial number as required by this chapter; or (j) to transport, deliver, or receive any firearm in interstate commerce which has not been registered as required by this chapter; or (k) to receive or possess a firearm which has been imported or brought into the United States in violation of section 5844; or (l) to make, or cause the making of, a false entry on any application, return, or record required by this chapter, knowing such entry to be false. |
post_count += 1
PGP: 912E3E9A194DED4E47DA0BA9D593AD70C8C12B9C
PGP: 912E3E9A194DED4E47DA0BA9D593AD70C8C12B9C
|
Originally Posted By scul: @CFletch @DFARM Looking at this more, and I'm pretty sure the marking requirements are still intact. Marking is required per 5842(a), and only 5842(b) and 5861(i) were enjoined by Jensen. As I read it, you can possess an unmarked can, but if you make it, the markings need to be applied CFletch, if you have further clarification on this, it would be much appreciated. I'd genuinely love to be shown that this reading is wrong. https://saf.org/wp-content/uploads/2026/08/TX-NFA-opinion.pdf (Last page) https://www.law.cornell.edu/uscode/text/26/5842 https://www.law.cornell.edu/uscode/text/26/5861 (b-f) enjoined by SSvATF Originally Posted By scul: Originally Posted By CFletch: Originally Posted By scul: Originally Posted By DFARM: Silly question that maybe someone in this thread has some ideas about. Are you guys worried about marking requirements? It looks to me like there might still be a need to mark home built cans because I believe there are non-tax related laws that require it Yea, the marking requirements were not enjoined, so I'm pretty sure you still have to mark them. I also assume you cannot use a Trust, unless the trust is somehow a member of GOA or another specified group. @CFletch @DFARM Looking at this more, and I'm pretty sure the marking requirements are still intact. Marking is required per 5842(a), and only 5842(b) and 5861(i) were enjoined by Jensen. As I read it, you can possess an unmarked can, but if you make it, the markings need to be applied CFletch, if you have further clarification on this, it would be much appreciated. I'd genuinely love to be shown that this reading is wrong. https://saf.org/wp-content/uploads/2026/08/TX-NFA-opinion.pdf (Last page) The Jensen plaintiffs are entitled to relief from two additional NFA provisions that only they challenge. See supra, n.10; 26 U.S.C. 5842(b), 5861(i). https://www.law.cornell.edu/uscode/text/26/5842 26 U.S. Code 5842 - Identification of firearms (a) Identification of firearms other than destructive devices Each manufacturer and importer and anyone making a firearm shall identify each firearm, other than a destructive device, manufactured, imported, or made by a serial number which may not be readily removed, obliterated, or altered, the name of the manufacturer, importer, or maker, and such other identification as the Secretary may by regulations prescribe. (b) Firearms without serial number Any person who possesses a firearm, other than a destructive device, which does not bear the serial number and other information required by subsection (a) of this section shall identify the firearm with a serial number assigned by the Secretary and any other information the Secretary may by regulations prescribe. (c) Identification of destructive device Any firearm classified as a destructive device shall be identified in such manner as the Secretary may by regulations prescribe. https://www.law.cornell.edu/uscode/text/26/5861 26 U.S. Code 5861 - Prohibited acts It shall be unlawful for any person (a) to engage in business as a manufacturer or importer of, or dealer in, firearms without having paid the special (occupational) tax required by section 5801 for his business or having registered as required by section 5802; or (b) to receive or possess a firearm transferred to him in violation of the provisions of this chapter; or (c) to receive or possess a firearm made in violation of the provisions of this chapter; or (d) to receive or possess a firearm which is not registered to him in the National Firearms Registration and Transfer Record; or (e) to transfer a firearm in violation of the provisions of this chapter; or (f) to make a firearm in violation of the provisions of this chapter; or (g) to obliterate, remove, change, or alter the serial number or other identification of a firearm required by this chapter; or (h) to receive or possess a firearm having the serial number or other identification required by this chapter obliterated, removed, changed, or altered; or (i) to receive or possess a firearm which is not identified by a serial number as required by this chapter; or (j) to transport, deliver, or receive any firearm in interstate commerce which has not been registered as required by this chapter; or (k) to receive or possess a firearm which has been imported or brought into the United States in violation of section 5844; or (l) to make, or cause the making of, a false entry on any application, return, or record required by this chapter, knowing such entry to be false. But I'm not a lawyer. I can't see why there would be any marking requirements at all if an item no longer has to be registered, since then it's no different than any other homemade firearm for personal use. |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. |
|
Originally Posted By memsu: Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. I print fiberon PA6-CF very successfully with the following settings: 100 bed 290-300 nozzle 65 chamber No fan except on extreme overhangs 100% rectilinear infill. Setting it to 99% gyroid will end up being nearly exactly the same as rectilinear anyway. I believe the 99% trick is a relic from the old days of cura where using 100% would cause issues with slicing and modern slicers can handle 100% just fine. A brim and some glue stick can help but I only use them maybe half the time. I know it's not what polymaker recommends but I have had much better results this way. I've printed several rimfire cans and a 9mm with zero warp or adhesion issues. I am using Prusas satin sheet. |
|
Originally Posted By Blob: I print fiberon PA6-CF very successfully with the following settings: 100 bed 290-300 nozzle 65 chamber No fan except on extreme overhangs 100% rectilinear infill. Setting it to 99% gyroid will end up being nearly exactly the same as rectilinear anyway. I believe the 99% trick is a relic from the old days of cura where using 100% would cause issues with slicing and modern slicers can handle 100% just fine. A brim and some glue stick can help but I only use them maybe half the time. I know it's not what polymaker recommends but I have had much better results this way. I've printed several rimfire cans and a 9mm with zero warp or adhesion issues. I am using Prusas satin sheet. Originally Posted By Blob: Originally Posted By memsu: Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. I print fiberon PA6-CF very successfully with the following settings: 100 bed 290-300 nozzle 65 chamber No fan except on extreme overhangs 100% rectilinear infill. Setting it to 99% gyroid will end up being nearly exactly the same as rectilinear anyway. I believe the 99% trick is a relic from the old days of cura where using 100% would cause issues with slicing and modern slicers can handle 100% just fine. A brim and some glue stick can help but I only use them maybe half the time. I know it's not what polymaker recommends but I have had much better results this way. I've printed several rimfire cans and a 9mm with zero warp or adhesion issues. I am using Prusas satin sheet. Before failure I did get higher in the print when I was printing enclosed than when I had it not enclosed. I also removed z hop because I didn't want to shake the print too much on a tall vertical print. I'm printing some small parts now to use up what I have left on this roll. Then I'll have to dry my other roll and give another shot at this later this week. |
|
Originally Posted By memsu: Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. Why not just spooljoin it? |
|
Originally Posted By memsu: Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. 3 walls, door closed, top glass in place, no cooling except at the print head, 300C nozzle, plate 50C, chamber 50C (for consistency), glue stick on plate No idea why you'd change the infill pattern |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
Originally Posted By CFletch: AI is bad and you shouldn't use it 3 walls, door closed, top glass in place, no cooling except at the print head, 300C nozzle, plate 50C, chamber 50C (for consistency), glue stick on plate No idea why you'd change the infill pattern Originally Posted By CFletch: Originally Posted By memsu: Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. 3 walls, door closed, top glass in place, no cooling except at the print head, 300C nozzle, plate 50C, chamber 50C (for consistency), glue stick on plate No idea why you'd change the infill pattern Your settings are basically what I had during the first print. I just printed some smaller Hoffman parts for the takedown pins because I wanted those in PA6 not PLA+ and parts for the U-DIS and those came out fine, but no where near the number of layers of the suppressor. It's like this Polymaker stuff isn't suited for my printer since it's insulated unlike my P1S which might end up having a lower chamber temp. I was hoovering about 58C in my QIDI Plus 4 for chamber temp. Now the Sunlu PA6 I ordered looks like it's meant to be printed in my QIDI Plus 4 printer. Requires much higher bed temp and chamber temps. |
|
Originally Posted By memsu: Your settings are basically what I had during the first print. I just printed some smaller Hoffman parts for the takedown pins because I wanted those in PA6 not PLA+ and parts for the U-DIS and those came out fine, but no where near the number of layers of the suppressor. It's like this Polymaker stuff isn't suited for my printer since it's insulated unlike my P1S which might end up having a lower chamber temp. I was hoovering about 58C in my QIDI Plus 4 for chamber temp. Now the Sunlu PA6 I ordered looks like it's meant to be printed in my QIDI Plus 4 printer. Requires much higher bed temp and chamber temps. Originally Posted By memsu: Originally Posted By CFletch: Originally Posted By memsu: Ok, time to reach out for some advice. I had to stop my FTN5 rimfire flow print again due to it coming loose from the build plate. It was still attached by the brim but the suppressor portion warped at the bottom. First layer is awesome and may be slightly a little low. For Polymaker PA6-CF printing at 290C, bed 50C, door cracked open, top glass removed, printing directly to bare PEI that I washed with Dawn soap before printing. Other than these changes using 300BlkFDE's print settings. I had it printing 6 walls, but now thinking the 3 walls they mentioned in guide might be better (they said more walls were optional), but what infill would you use? AI was telling me 99% Gyroid would help relieve the stress inside the part vs using rectilinear etc. AI also suggested a lower bed temperature and trying Magigoo PA on the bed. It might appear my insulated printer is working against me with the Polymaker formula they use. I ordered a roll of Sunlu PA6-CF to better use my insulated heated chamber in my QIDI Plus 4. I'd try printing on my Bambu P1S with the Polymaker, but i need to order a hardened extruder for it. I don't have enough filament on this roll to print another suppressor, so might just use rest of it up printing some small nylon parts I need. 3 walls, door closed, top glass in place, no cooling except at the print head, 300C nozzle, plate 50C, chamber 50C (for consistency), glue stick on plate No idea why you'd change the infill pattern Your settings are basically what I had during the first print. I just printed some smaller Hoffman parts for the takedown pins because I wanted those in PA6 not PLA+ and parts for the U-DIS and those came out fine, but no where near the number of layers of the suppressor. It's like this Polymaker stuff isn't suited for my printer since it's insulated unlike my P1S which might end up having a lower chamber temp. I was hoovering about 58C in my QIDI Plus 4 for chamber temp. Now the Sunlu PA6 I ordered looks like it's meant to be printed in my QIDI Plus 4 printer. Requires much higher bed temp and chamber temps. Use some glue stick, that is key. With the above method I've printed almost a dozen tall prints with only 1 breaking free (and that was immediate, not many layers into the print, because of a partially clogged nozzle not outputting the filament properly). |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
I'm about 20 layers away from being done with all my planned 3D2A stuff, at least unless something else explodes or breaks upon testing. I'll run an annealing batch for the last couple of weeks of prints tonight, and then I'll just need to find some time to go test them. Is moisture conditioning actually needed after annealing? |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
Originally Posted By CFletch: I'm about 20 layers away from being done with all my planned 3D2A stuff, at least unless something else explodes or breaks upon testing. I'll run an annealing batch for the last couple of weeks of prints tonight, and then I'll just need to find some time to go test them. Is moisture conditioning actually needed after annealing? |
|
Originally Posted By D_Man: Annealing will basically re-dry the nylon, making it more brittle. It would be a good idea to allow something like PA6 to rehydrate a bit to get back that slight "springiness" that gives it strength, especially in something like a can which will see impact forces from the pressure of the expanding gases. Originally Posted By D_Man: Originally Posted By CFletch: I'm about 20 layers away from being done with all my planned 3D2A stuff, at least unless something else explodes or breaks upon testing. I'll run an annealing batch for the last couple of weeks of prints tonight, and then I'll just need to find some time to go test them. Is moisture conditioning actually needed after annealing? |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
Originally Posted By CFletch: Any recommendations for method?  If you're someplace naturally dry, you can put it into a zip lock bag or sealable food container with a moist towel or sponge inside (but not touching the part) as well for a few days. |
|
Originally Posted By D_Man: This time of year, I just let the part sit in my 70+% RH basement for a few days or a week. If you're someplace naturally dry, you can put it into a zip lock bag or sealable food container with a moist towel or sponge inside (but not touching the part) as well for a few days. Originally Posted By D_Man: Originally Posted By CFletch: Any recommendations for method? If you're someplace naturally dry, you can put it into a zip lock bag or sealable food container with a moist towel or sponge inside (but not touching the part) as well for a few days. |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
Originally Posted By mvintx: ziploc bag, wet sponge, two weeks conditioning time You spent all the time researching and printing, be patient and it will pay off. I don't think you need to wait two weeks with the sponge and bag method. Two or three days is probably fine. |
|
Originally Posted By blwngazkit: Has anyone tried any of the newer 3d Resins from Inslogic, Loctite, Liqreate? Some of the newer resins are pretty impressive, still no where close to PA6-CF or PPA-CF. I'm picturing printing baffles or a baffle stack to stick in a metal tube... No resin of any type is suitable for 3D2A |

|
Here are the FTN6 K can and the 8 in boosted PA6-GF Attached File Attached File Attached File Threads were a little rough, needed a tap run through. Attached File Attached File |
|
Originally Posted By Blob: No resin of any type is suitable for 3D2A Some of the newer resins are roughly equal to PLA is specs, and many of the 3D2A designs began as PLA prints. I think I'm going to be doing some testing just to satisfy my curiosity. |
|
Originally Posted By DANGERRUSS: Here are the FTN6 K can and the 8 in boosted PA6-GF https://www.ar15.com/media/mediaFiles/126580/IMG_8515_jpeg-3814125.JPG https://www.ar15.com/media/mediaFiles/126580/IMG_8513_jpeg-3814126.JPG https://www.ar15.com/media/mediaFiles/126580/IMG_8516_jpeg-3814127.JPG Threads were a little rough, needed a tap run through. https://www.ar15.com/media/mediaFiles/126580/IMG_8514_jpeg-3814128.JPG https://www.ar15.com/media/mediaFiles/126580/IMG_8518_jpeg-3814129.JPG Looks wet and underextruded |
|
I've come to the conclusion that you can't follow Polymaker's bed temp and chamber temp recommendations (40-50C bed and ambient) with PA6-CF. Previously I printed at 40C, 45C, and 50C bed temps (chamber open) no fans and 290-300C. Now I've upped it to 100C bed and 65C chamber temp. I've been trying to use up my roll from 2 failed FTN5 Rimfire Flow print failures and print other items I needed that would be good to have in nylon. I've printed Scarpion replacement parts for the PLA+ ones I had, parts for the U-DIS, and some M-Lok covers that printed vertical with very little bed contact. All that was successful and had no warping even on the thin rail covers. I did up my first layer from 0.15mm to 0.2mm as well. I've got my last roll of Polymaker PA6-CF in the dehydrator right now, so I'll try running hot this go around and see how it does. I also bought some Magigoo PA to put on my PEI bed. |
|
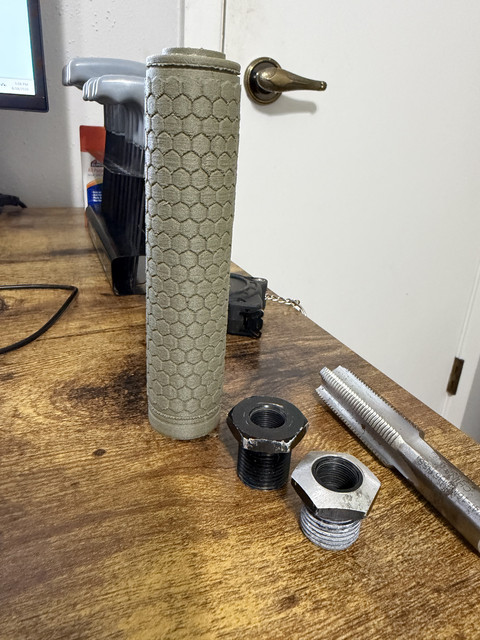
Originally Posted By Network_Daddy: Direct threading a PLA can on a 22 pistol. Bad idea?
|
|
Originally Posted By Network_Daddy: Direct threading a PLA can on a 22 pistol. Bad idea? Works fine. The three things to keep in mind are (1) - correct calibration and/or use of "X/Y hole compensation" so the threads aren't undersized and tight (2) - PLA on a can, especially a pistol can, calls for slow rate of fire regardless. Like... I've done 20-round rapid fire of minimags from a 4.5" barrel with minimal effect to the PLA-plus blast baffle, but that's something you'd definitely want to let things cool down before you went to town again. If you're looking to get rowdier, PLA is not the right choice regardless of threading method. (3) If people are worried about alignment, print hot and slow to avoid wobbles and for extra strength. Check the alignment, if it's off, your printer is out of square and you should fix it. I have a decent gaggle of Form-1'd, 3d-printed cans. I've used a thread adapter on one (actually one of these). But aside from "it's a little easier to spin on", it doesn't add enough benefit for me to keep down that route, I just print direct-thread cans. I get the appeal of a fancier print. But with this filament working just fine and costing me about $1 per suppressor... it's hard for me to get excited about spending more money and time. I can get a form 1 submitted in something like 2-3 minutes, so 3 minutes of time and $1 in filament... when a can wears out, doesn't bother me at all to throw it in the trash. If I felt like getting fancier on the cans, I'd probably use something like this (or another brake, with or without a blast shield) and get a steel blast baffle out of the deal as well. |
|
Originally Posted By DANGERRUSS: Fresh from package I dried it @ 100c for 12 hrs and lowered the temp to 85c during the prints, so another 20 hrs. Then you have some other issues. Here are some threads I printed in PA6-CF over the last couple days. No clean up needed. Attached File Attached File Attached File Attached File |

|
So, first dumb question here - Currently running a Flashforge AD5X, and have it pretty well dialed in with PLA+. Now, i know PA6-CF (of which i have two spools coming) is the hot shit; but how much would i regret playing with an FTN 5.1 Flow on my PTR9? No FRT, casual shooting. The documents say it can survive (direct quote: "PPA-CF or PA-CF are preferred, but it'll survive in PLA+. ", but I am curious how much people may have actually used it. |
|
Originally Posted By CFletch: If 5861 b-f are enjoined by SS, that would seem to be sufficient on its own for making a suppressor without the SN. Jensen would then cover possessing or receiving such a suppressor. But I'm not a lawyer. I can't see why there would be any marking requirements at all if an item no longer has to be registered, since then it's no different than any other homemade firearm for personal use. Originally Posted By CFletch: Originally Posted By scul: Originally Posted By CFletch: Originally Posted By scul: Originally Posted By DFARM: Silly question that maybe someone in this thread has some ideas about. Are you guys worried about marking requirements? It looks to me like there might still be a need to mark home built cans because I believe there are non-tax related laws that require it Yea, the marking requirements were not enjoined, so I'm pretty sure you still have to mark them. I also assume you cannot use a Trust, unless the trust is somehow a member of GOA or another specified group. @CFletch @DFARM Looking at this more, and I'm pretty sure the marking requirements are still intact. Marking is required per 5842(a), and only 5842(b) and 5861(i) were enjoined by Jensen. As I read it, you can possess an unmarked can, but if you make it, the markings need to be applied CFletch, if you have further clarification on this, it would be much appreciated. I'd genuinely love to be shown that this reading is wrong. https://saf.org/wp-content/uploads/2026/08/TX-NFA-opinion.pdf (Last page) The Jensen plaintiffs are entitled to relief from two additional NFA provisions that only they challenge. See supra, n.10; 26 U.S.C. 5842(b), 5861(i). https://www.law.cornell.edu/uscode/text/26/5842 26 U.S. Code 5842 - Identification of firearms (a) Identification of firearms other than destructive devices Each manufacturer and importer and anyone making a firearm shall identify each firearm, other than a destructive device, manufactured, imported, or made by a serial number which may not be readily removed, obliterated, or altered, the name of the manufacturer, importer, or maker, and such other identification as the Secretary may by regulations prescribe. (b) Firearms without serial number Any person who possesses a firearm, other than a destructive device, which does not bear the serial number and other information required by subsection (a) of this section shall identify the firearm with a serial number assigned by the Secretary and any other information the Secretary may by regulations prescribe. (c) Identification of destructive device Any firearm classified as a destructive device shall be identified in such manner as the Secretary may by regulations prescribe. https://www.law.cornell.edu/uscode/text/26/5861 26 U.S. Code 5861 - Prohibited acts It shall be unlawful for any person (a) to engage in business as a manufacturer or importer of, or dealer in, firearms without having paid the special (occupational) tax required by section 5801 for his business or having registered as required by section 5802; or (b) to receive or possess a firearm transferred to him in violation of the provisions of this chapter; or (c) to receive or possess a firearm made in violation of the provisions of this chapter; or (d) to receive or possess a firearm which is not registered to him in the National Firearms Registration and Transfer Record; or (e) to transfer a firearm in violation of the provisions of this chapter; or (f) to make a firearm in violation of the provisions of this chapter; or (g) to obliterate, remove, change, or alter the serial number or other identification of a firearm required by this chapter; or (h) to receive or possess a firearm having the serial number or other identification required by this chapter obliterated, removed, changed, or altered; or (i) to receive or possess a firearm which is not identified by a serial number as required by this chapter; or (j) to transport, deliver, or receive any firearm in interstate commerce which has not been registered as required by this chapter; or (k) to receive or possess a firearm which has been imported or brought into the United States in violation of section 5844; or (l) to make, or cause the making of, a false entry on any application, return, or record required by this chapter, knowing such entry to be false. But I'm not a lawyer. I can't see why there would be any marking requirements at all if an item no longer has to be registered, since then it's no different than any other homemade firearm for personal use. b-d deal with receiving or possessing a firearm made in violation, but not making. That's the part that I think needs determination how these interplay - not that I'm going to send a letter to the ATF about this. I'm not lawyer either, but I am also hopeful the marking requirements are moot. |
post_count += 1
PGP: 912E3E9A194DED4E47DA0BA9D593AD70C8C12B9C
PGP: 912E3E9A194DED4E47DA0BA9D593AD70C8C12B9C
|
Originally Posted By ENGCPT: For those of you who keep having prints fail when they get to tall, is there a reason you cant print the device on its side? It may be a stupid question but im still in the research before I buy stage. It's the orientation recommended by the designers. Some can be printed upright and some need to be printed sideways and at an angle. I think I finally figured out my settings for Polymaker PA6-CF for my printer. You have to keep the bed temp and chamber temp as close as possible. I also obtained some Magigoo PA to put on the bed to help it hold the PA6 better to my PEI sheet. Right now with 1.5 hours remaining it's looking good for my FTN5 Rimfire Flow. This is my 4th attempt at one. |
|
Originally Posted By ENGCPT: For those of you who keep having prints fail when they get to tall, is there a reason you cant print the device on its side? It may be a stupid question but im still in the research before I buy stage. The cans are designed to be strong in specific layer directions, and you do not want to deviate from those. If it is designed for sideways, print sideways. If designed for upright, print upright. |
Participation in the rights of citizenship presumes participation in the duties of citizenship
|
Originally Posted By ENGCPT: For those of you who keep having prints fail when they get to tall, is there a reason you cant print the device on its side? It may be a stupid question but im still in the research before I buy stage. The way the layers are stacked plays an enormous role in how strong the part is since layer adhesion is the weakest link, and suppressors are designed from the beginning with a specific orientation in mind in order to maximize strength. Printing them on their side could affect the can's properties and you'll have to deal with overhangs that weren't present before. I would recommend always printing them in the intended orientation unless you really know what you're doing. If you're having trouble with prints coming loose then you need to solve that problem. |
|
Originally Posted By ENGCPT: For those of you who keep having prints fail when they get to tall, is there a reason you cant print the device on its side? It may be a stupid question but im still in the research before I buy stage. I switched to the engineering plate and glue, increased the brim size by 5mm and haven't had a problem since. |
"Fully-loaded, safety off. This here is a recipe for unpleasantness." - Malcom Reynolds
"He's a precision-guided asshole who only deploys on deserving targets." - Grok
"He's a precision-guided asshole who only deploys on deserving targets." - Grok
Easily irritated engineer of odd things
Joined:
Jul 2008
Posts:
32084
EE: 100% (5)
 MN, USA
|
Nano Polymer Adhesive is the gold standard of bed adhesion products. Yes, it is kind of expensive, but it goes a LONG way and lasts a while. I'm still on my first bottle from a few years ago. |
Once you realize that all power comes from the credible threat of the use of deadly force, and the gov't hates you, most things become easy to understand..
| speaking of glue sticks, any suggestions for cleaning a textured PEI plate that has a few dozen layers of glue on it? Is there some chemical that will eat it all off without damaging the plate? |
Participation in the rights of citizenship presumes participation in the duties of citizenship

|
Originally Posted By Blob: Then you have some other issues. Here are some threads I printed in PA6-CF over the last couple days. No clean up needed. https://www.ar15.com/media/mediaFiles/160722/1000021742_jpg-3814543.JPG https://www.ar15.com/media/mediaFiles/160722/1000021741_jpg-3814544.JPG https://www.ar15.com/media/mediaFiles/160722/1000021740_jpg-3814545.JPG https://www.ar15.com/media/mediaFiles/160722/1000021743_jpg-3814546.JPG Damn, those are beautiful threads...mine don't look anything like that. I think I've got my calibration pretty well dialed in but I still get globs in the threads. Just got my Comstock hub adaptor and it does not thread easily into my test piece. Takes a pair of channel locks and a socket wrench. Need to do the X-Y hole compensation. |