


Armory Sponsor


Posted: 3/8/2010 6:17:52 AM EDT
|
Finally going to get around to crowning my .223 barrel on my Savage 10FP. This one started as a sporter weight that I cut down. I tried the Brownells cutter, but just isn't working out, need to cut it in the lathe.
We have a small 8 by 30 Clausing with a 3 jaw and a steadyrest. From what I've read, I should made a bushing with an ID taper for the barrel to ride in the steady. Do I need to find the 4 jaw for the chamber end, or will the 3 be good enough? Just how close should the muzzle runout be? I know 0 would be ideal, but is there an acceptable range? Probably have more questions, but I'll start here 
thanks for the help guys 
|
| It would probably be more exact if you're able to lock the muzzle end of the barrel in a 4 jaw and the chamber/breech end of the barrel through the other side of the headstock in a 3 jaw. Steady rests are nice, but they're not that precise. As far as an acceptable amount of runout, as close to zero as possible, I realize that it might not be possible to get perfect zero, but about a half a thousandth or so runout isn't anything to get worked up about. |
|
Depends on the 3 jaw. I have used shim stock between a part and one of the jaws on a three jaw, to get a part to run true, when a 4 jaw wasn't available.
Will you be checking the runout on the ID? Instead of worrying about a steady and chucking the receiver. Can you get the barrel through the headstock, and use a Cat's paw to keep the receiver or barrel centered? Where are you located? |
|
If it were me and I could get the bbl through the headstock, I'd use a cat's head on the outside end and have as little overhang as possible on the chuck side. Use a gage pin in the bore to indicate for 0-0 runout, or maybe a half thousandth at most. Use brass/aluminum shim stock between the barrel and chuck jaws to keep from marring it up.
If you don't have a four jaw, it's pretty easy to make a cat's head from some heavy wall pipe and capscrews....just use brass shim stock between the screws and the barrel. |
|
I'll have to check again, but I think the headstock was 20" and my barrel is 18". And there's no place to attach a cats paw either. Think I'm limited to the 3 or 4 jaw and steadyrest.
Can I indicate the bore directly, or should I turn a small gage spud to indicate? Not too worried if it doesn't come out perfect, only paid $40, I can always redo it. Gun Crank, I'm up in Hibbing. Shop is kinda lmited for odd jobs, setup for production of rock bits. But I do what I can. |
|
I'd use a gauge pin like machinisttx recommended. If you were close I'd lend you mine. you could turn a spud. I wouldn't indicate off the OD.
I have turned long shafts without a catspaw. I made a light press fit plastic bushing that fit into the back of the headstock. I held .001 TIR on those parts. I'd love to move up north. Don't know how busy I'd stay in the shop though. |
The bushing idea may work out. I did manage to find the 4 jaw, cleaning it up now, think it has about 15 years of dust on it, no kidding 
Found a spud I made before, nice snug slip to the bore, so I can indicate on that. Looks like progress 
I spent 7 years living in Coon Rapids/Blaine working in the EDM dept at Dynamic Engineering. Can't say I miss it too much, tho it was nice to have the Wires and Sinkers at my disposal 
|
|
Well got it done, thanks for all the help guys
Used the tape trick, since the spindle bore seemed tapered and the breech end ended up in the middle somewhere. Had to cut a feeding ramp so it wouldn't keep jamming bullets .040 low of the chamber. Cut the feed cone first, setup for the crown second. Got it dialed in within .0002. Looks good to me, here's some pics 
Feed cone setup 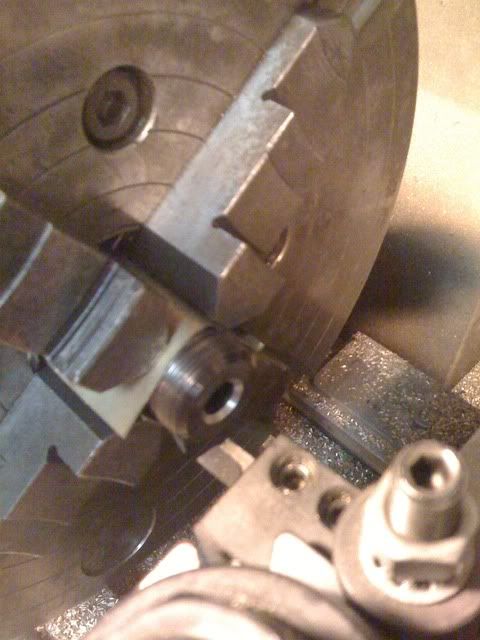
Crown setup 
Feedcone and crown 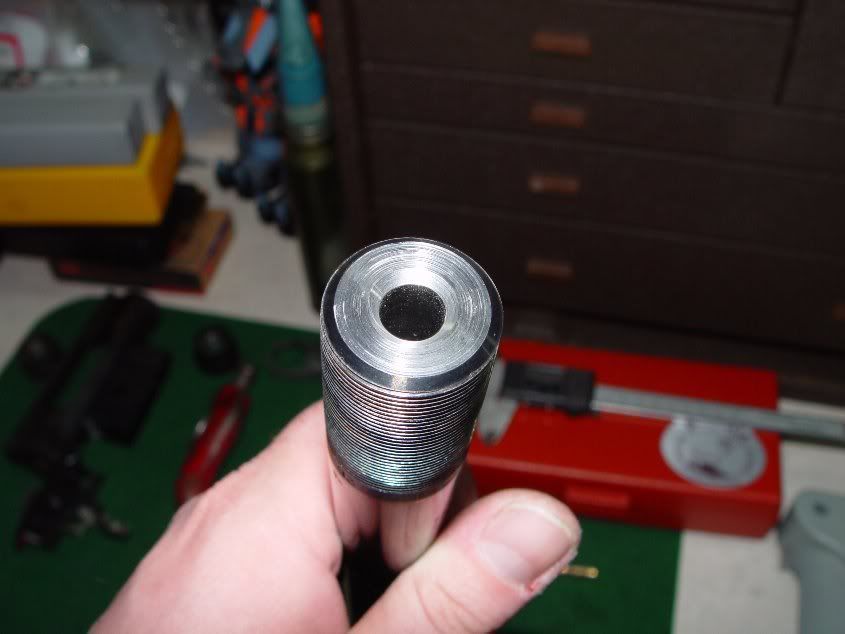

The Savage it's on, need to get her sighted in and whack some coyotes I've been hearing 
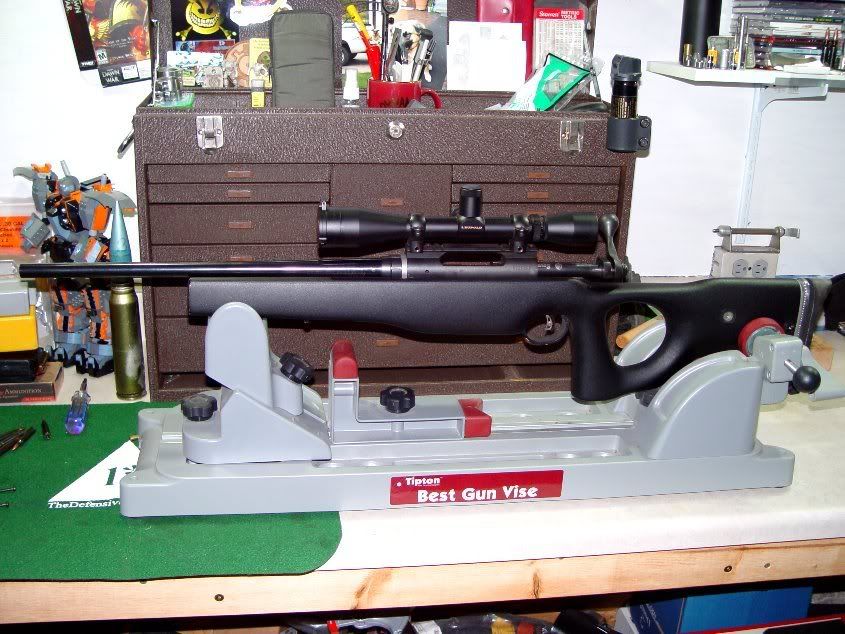
|
|
Well, if you had been cutting an 11degree, or conventional rounded edge crown, all that precision would have been well worth taking.
Correct me if I'm wrong (always a possibility with me) but the picture looks like a recessed 90 degree crown. In which case, I think working to 2 "tenths" is overkill. A nice clean cut at 90 degrees is what's needed, concentricity is a minor consideration (IMO)with such a crown. The job looks good though! Don in Ohio |
Armory Sponsor
Join the Community
Your next conversation starts here.
Create your free account to join discussions, share your experience, save topics, and connect with the AR15.COM community.
- Join discussions
- Follow topics and replies
- Connect with fellow enthusiasts
Already a member? Sign in
Stay informed by subscribing to our Newsletter