


The thread for new to 3D printing to ask questions (Page 1 of 7)
Posted: 2/27/2026 12:15:31 PM EDT
[Last Edit: turtle2472][Edited]
|
ETA: For anyone who found this thread thanks to the Newsletter, welcome! I highly recommend reading through the pinned threads in this subforum. Also, -Obsessed- did a great thread on helping set expectations for 3D printing. I highly recommend checking it out too. I've been asking my questions in random threads that lends to thread sliding. Rather than that I figure it is best if I go ahead and start a thread where I can ask all my random questions to try to get some feedback. I'm not the only new to 3D printing user here so I figure it can be a general free for all to get general help and pointers from users who are way more versed in 3D printing. I've had my printer for just over three weeks now and only printed with PLA from Bambu Labs until today when my ABS finally dried. I've now had two print failures out of the multiple prints I've done. The first, I'm not sure what happened. Adhesion of the left foot is my best guess, but the support for the mask ties broke during printing too. In the time-lapse you can see the foot separate and then the strings going everywhere. I'm actually impressed it was able to finish as much of the build as it did after losing that foot!    I haven't messed with that print again so I'll get around to trying it again later. Yesterday my Sunlu ABS was delivered. It spent 16 hours in my AMS 2 Pro on drying to make sure it was cooked. I loaded it and printed a heat deflector for my P2S. I happened to be watching it print and saw it curling on the edges (not adhering to the plate) and then completely separate from the bed and start spinning around.  Since I was watching, I was able to stop the job and see if I could figure out the problem. PEI plate needs glue for ABS. I'm digging around but struggling to find a good answer. What kind of glue stick other than ones from Bambu Labs? Or, other options if not glue. I saw hairspray recommended. ETA: For printing with ABS, is my problem I didn't run calibrations again since switching my spools out to ABS? |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By Blob: What are you bed and chamber temps? Wash your build plate thoroughly with hot water and dish soap. I don't use glue stick with any material and don't have problems with bed adhesion. I don't know for sure. :embarrassed: It is a Makerworld job that I pressed print. (To be honest, most of my jobs are like that because I have little clue about what I'm doing.). For the print profile I picked P2S and ABS Deflector. IIRC the plate was 90° and chamber was heated, but I don't recall to what. Wash the build plate? Also embarrassed here. I haven't washed it since I got it. Haven't flipped it over either. I've fixed that now. It is drying on the dish rack. You may all point and laugh at me now. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: I don't know for sure. :embarrassed: It is a Makerworld job that I pressed print. (To be honest, most of my jobs are like that because I have little clue about what I'm doing.). For the print profile I picked P2S and ABS Deflector. IIRC the plate was 90° and chamber was heated, but I don't recall to what. Wash the build plate? Also embarrassed here. I haven't washed it since I got it. Haven't flipped it over either. I've fixed that now. It is drying on the dish rack. You may all point and laugh at me now. It's ok we all start somewhere. 90 bed is on the low end for ABS. I run mine at 110 with 55C chamber and don't have warp or adhesion issues. Higher chamber temps are critical to keep ABS from warping, just make sure that the printer reaches temp before it starts the print. Keeping the build plate clean is important. It's the first thing I do to a new sheet and I wash it periodically. Avoid touching the print area with your hands to keep oils from causing issues. |
|
The P2S doesn't have an actively heated chamber. This is the same complaint I have in Prusa Core machines. You are going to be fighting with ABS and ASA forever as you don't have a way to control chamber heat. The general consensus is jack the heat bed way up which does help keep the chamber hotter and increases adhesion but it also increases internal part stress and warp force. I print at a 65C chamber and 90C bed and thus far, after about 250 hrs of printing ABS only, I've not had a single part warp or pop off mid print. Try the bed temp to see if it can get your chamber to a MINIMUM of 50C, 55C is better. Truly 65C is ideal but only really needed on larger parts, and Squirtle isn't that big.  Get a blanket, insulation panels, etc, to see if that can help get the chamber temp up. The P2S can monitor chamber temp but it cannot control it directly. |
|
Originally Posted By turtle2472: I don't know for sure. :embarrassed: It is a Makerworld job that I pressed print. (To be honest, most of my jobs are like that because I have little clue about what I'm doing.). For the print profile I picked P2S and ABS Deflector. IIRC the plate was 90° and chamber was heated, but I don't recall to what. Wash the build plate? Also embarrassed here. I haven't washed it since I got it. Haven't flipped it over either. I've fixed that now. It is drying on the dish rack. You may all point and laugh at me now. Don't air dry it. Blow it off with dry compressed air if you can, or a lint free cloth if you can't. Aside from Zero Water and RO/distilled water, you'll have dissolved solids which if allowed to air dry will be left in the plate, making it dirty. |
|
Originally Posted By -Obsessed-: also increases internal part stress and warp force. Citation? One would think that keeping as much of the part as possible closer to printed temp would reduce stress which is why high chamber temps are necessary. Cooling is what's causing the warpage. Like how annealing at high heat reduces stress and why hot rolled steels have less stress than cold rolled. |
|
Success! I set the plate to 110°C and the chamber did what it did. I thought it had active heat, but I guess it is just recirculation. At start the chamber was 35°C and it was 46°C at the end of the 26 minute print. It stayed on the plate and is still there while it cools down. I didn't even open the chamber (though it was tempting) so it could cool evenly and slowly. I also saw the note to blow off my plate rather than air drying and did that too! I'm sure my dirty plate contributed to the lack of adhesion. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By Blob: Citation? One would think that keeping as much of the part as possible closer to printed temp would reduce stress which is why high chamber temps are necessary. Cooling is what's causing the warpage. Like how annealing at high heat reduces stress and why hot rolled steels have less stress than cold rolled. I'd have to find it, it was a white paper on the subject of 3DP and stresses encountered on parts both during and after printing. I stumbled across it trying to find research on infill strengths relative to wall counts. The premise was that you want the lowest bed temp that effectively sits inside the Tg of the filament, because you introduce further stress by having a higher gradient between layer 1 and 2, and 2 to 3, and 3 to 4, and these gradients compound stress forces and will percolate further up the print, as on a normal 90C bed, the stresses are going about 10mm and at a 110C bed the stresses go like 13 or 14, and that leverage compounds. While adhesion is gained, stresses also increase as ultimately the total gradient and thus stresses in the part at any point in time are 90C to 65C vs 110C to 65C (or whatever your chamber temp is). It's the same reason cooler chambers have more stress on parts, as it increases the absolute gradient magnitude between layer one and the top layer. It was written by PhDs but made sense to me anyway. I can see the thermodynamics playing out that way. |
 I can stop any time. I don't have a problem at all.  My 10 pack of Sunlu PETG got delivered today. I've taken the ABS out of the AMS and put in PETG to dry now. After it runs for 12 hours I'll try to print something with it. I went with the Black, Red, White, and Blue for this load. :) Seems like a good start for being a little over three weeks in. I have options for sure! |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
New question: When my Sunlu ASA comes in, am I going to have issue printing it with the P2S? I got it because I really need something like this for outdoor signs and such for our homestead and ASA seems to be the best fit for it. It hasn't shipped yet though so if I'm going to struggle, I can cancel the order now before it does ship. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: New question: When my Sunlu ASA comes in, am I going to have issue printing it with the P2S? I got it because I really need something like this for outdoor signs and such for our homestead and ASA seems to be the best fit for it. It hasn't shipped yet though so if I'm going to struggle, I can cancel the order now before it does ship. It's not any harder than ABS. Actually most consider ASA more forgiving. I think the biggest factor in whether you'll be successful is part geometry. Large parts, tall, long straight edges, etc compound warp stresses. I'd say most would say a chamber in the 40s is generally too low for optimal strength for either ABS or ASA but some techniques can at least give you a successful print. Personally I'd still insulate it if you can. Nice storage. I just finished my cereal wall myself. Still printing the desiccant containers. Out of ABS ironically.  Attached File Attached File |

|
Unless you're printing in a controlled environment during winter, not sure how people are getting 50+C in the chamber. My printer is in the garage and I needed to add a heater to raise the chamber temp to print ASA, PC and PETG-CF. I used a Amazon Basics heater and a simple temp controller to regulate on/off of the heater. Printer Heater |
|
Originally Posted By -Obsessed-:It's not any harder than ABS. Actually most consider ASA more forgiving. I think the biggest factor in whether you'll be successful is part geometry. Large parts, tall, long straight edges, etc compound warp stresses. I'd say most would say a chamber in the 40s is generally too low for optimal strength for either ABS or ASA but some techniques can at least give you a successful print. Personally I'd still insulate it if you can. Nice storage. I just finished my cereal wall myself. Still printing the desiccant containers. Out of ABS ironically. https://www.ar15.com/media/mediaFiles/467079/12409_jpg-3720514.JPG https://www.ar15.com/media/mediaFiles/467079/12456_jpg-3720515.JPG Cool. I'm looking forward to trying out the ASA for the signs. I'm sure most of what I print with it will be flat and thin so hopefully not a problem. Think, placards. Some with holes and some with stakes on the bottom. Not that I won't print other things with it too, but signage is my big focus for it right now. I love your storage wall! I went with the Sterilite containers because they are only ~$7 a container and can hold 4 spools. Print off the stands and add 1/2" PVC pipe to hold them. I'm going to used the PETG to print corner desiccant holders for the bottom. When/if I do the cereal box set up like yours, I would want the bases you're using. I have spool hole desiccant holders for now since they will move around with them. The ones I have right now are PLA though and in another thread I jumped in I was told they would likely glass over during drying, so I'll print new ones that I can dry in. I'm also going to print some slide in holders for my AMS... I was talking with my wife about this printer and how out of my jobs have been for the printer or in support of the printer! Oh... then I'm thinking, do I get another AMS2 or just a filament dryer? If I get another AMS I can have a broader range of filament available. I already know an HT is in the future at some point. I'm glad I'm loving this hobby!
|
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By 67Cuda: Unless you're printing in a controlled environment during winter, not sure how people are getting 50+C in the chamber. My printer is in the garage and I needed to add a heater to raise the chamber temp to print ASA, PC and PETG-CF. I used a Amazon Basics heater and a simple temp controller to regulate on/off of the heater.  How did you get that in your printer? I love the idea here. Link to the actual heater? |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By 67Cuda: Unless you're printing in a controlled environment during winter, not sure how people are getting 50+C in the chamber. My printer is in the garage and I needed to add a heater to raise the chamber temp to print ASA, PC and PETG-CF. I used a Amazon Basics heater and a simple temp controller to regulate on/off of the heater. Printer Heater What printer do you have? I've observed 57C chamber with a 110 bed in my core ones in my office which is a constant 68-70F. No extra insulation. |
|
Originally Posted By turtle2472: I thought it had active heat, but I guess it is just recirculation. Have you googled fan settings for 3D printing ABS? Your auxiliary fan should be off for ABS. And your part cooling fan should be off or at a very low speed and speed up a little while doing an overhang or bridging. |
|
Originally Posted By 67Cuda:I actually made a simple YouTube video on what I did. https://youtu.be/S-GBlnI1bAQ?si=Y5A59k2DTrMKNEhG Thanks for sharing the video of it. I'm definitely not ready to cut a hole in the wall of my printer yet. I mean, it is just 3 weeks old right now. Give me two more and maybe! I did print with my PETG today and it is working out great. I just did default "Generic PETG" in my AMS and it is printing perfectly so far. My chamber is only 40°C with the bed being 70°C. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”

|
Originally Posted By -Obsessed-: Don't air dry it. Blow it off with dry compressed air if you can, or a lint free cloth if you can't. Aside from Zero Water and RO/distilled water, you'll have dissolved solids which if allowed to air dry will be left in the plate, making it dirty. |
Who, What, Where? Call Sign, Snowball
|
Originally Posted By turtle2472: Cool. I'm looking forward to trying out the ASA for the signs. I'm sure most of what I print with it will be flat and thin so hopefully not a problem. Think, placards. Some with holes and some with stakes on the bottom. Not that I won't print other things with it too, but signage is my big focus for it right now. I love your storage wall! I went with the Sterilite containers because they are only ~$7 a container and can hold 4 spools. Print off the stands and add 1/2" PVC pipe to hold them. I'm going to used the PETG to print corner desiccant holders for the bottom. When/if I do the cereal box set up like yours, I would want the bases you're using. I have spool hole desiccant holders for now since they will move around with them. The ones I have right now are PLA though and in another thread I jumped in I was told they would likely glass over during drying, so I'll print new ones that I can dry in. I'm also going to print some slide in holders for my AMS... I was talking with my wife about this printer and how out of my jobs have been for the printer or in support of the printer! Oh... then I'm thinking, do I get another AMS2 or just a filament dryer? If I get another AMS I can have a broader range of filament available. I already know an HT is in the future at some point. I'm glad I'm loving this hobby! Originally Posted By turtle2472: Originally Posted By -Obsessed-:It's not any harder than ABS. Actually most consider ASA more forgiving. I think the biggest factor in whether you'll be successful is part geometry. Large parts, tall, long straight edges, etc compound warp stresses. I'd say most would say a chamber in the 40s is generally too low for optimal strength for either ABS or ASA but some techniques can at least give you a successful print. Personally I'd still insulate it if you can. Nice storage. I just finished my cereal wall myself. Still printing the desiccant containers. Out of ABS ironically. https://www.ar15.com/media/mediaFiles/467079/12409_jpg-3720514.JPG https://www.ar15.com/media/mediaFiles/467079/12456_jpg-3720515.JPG Cool. I'm looking forward to trying out the ASA for the signs. I'm sure most of what I print with it will be flat and thin so hopefully not a problem. Think, placards. Some with holes and some with stakes on the bottom. Not that I won't print other things with it too, but signage is my big focus for it right now. I love your storage wall! I went with the Sterilite containers because they are only ~$7 a container and can hold 4 spools. Print off the stands and add 1/2" PVC pipe to hold them. I'm going to used the PETG to print corner desiccant holders for the bottom. When/if I do the cereal box set up like yours, I would want the bases you're using. I have spool hole desiccant holders for now since they will move around with them. The ones I have right now are PLA though and in another thread I jumped in I was told they would likely glass over during drying, so I'll print new ones that I can dry in. I'm also going to print some slide in holders for my AMS... I was talking with my wife about this printer and how out of my jobs have been for the printer or in support of the printer! Oh... then I'm thinking, do I get another AMS2 or just a filament dryer? If I get another AMS I can have a broader range of filament available. I already know an HT is in the future at some point. I'm glad I'm loving this hobby! With my FlashForge printer, I'd max out the bed temp for 30-45 minutes before starting a print in ASA or ABS to build up some extra heat in the chamber (that wasn't heated). H2D has solved that particular frustration. External dryer or AMS2? Get both....lol. I've got 1 AMS2 and 2 HT's hooked up to my H2D....I have an external dryer that I used with my old printer and I still use it. If I've got a print running (most of the time) it's easier to just throw the spools in the external dryer. That being said, I plan on adding another AMS2 to my H2D, simply so I don't have to move spools around as much.....unless I go ahead and buy the P2S with AMS2.
|
EP429: Today's lesson - Don't provoke ARFCOM. People will see your butthole.
|
I looked at getting another AMS2 but they are out of stock now so I'm going to hold off. It was going to be that AND two power adapters. One of the other threads mentioned needing to have the external power supply to best use them. More questions: When does BBL ever actually have filament in stock? Every time I look at buying some they are out. With bulk buying they are about the same price as others on Amazon but they never seem to have stock. Plus, as silly as it is, I'd like to get the RFID chips from some of them to make loading filament into the AMS simpler. If it is there, I would like to be able to use it without having to manually program it. Second question is how often should I actually wash my build plate? I do not touch it, ever. I printed a PLA scraper and flex it using the edge tabs. Speaking of RFID, can I get a repo of someone reading the chips so I can just clone them onto NFC/RFID tags I got from Amazon? I'm thinking something like these I got a long time ago. I'm wondering if there is a repo out there that has the data from the BBL spool chips that I can clone onto the NFC chips. I've got a ton of them from home automation things I use them for. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: Second question is how often should I actually wash my build plate? I do not touch it, ever. I printed a PLA scraper and flex it using the edge tabs. Depends. My satin sheet at work hasn't been washed since May or June of last year and it's still working perfectly fine. I am careful about not touching the print area but I do handle it by the edges. When I snap a print off I will put my fingers on the edges and bottom side of the sheet to flex it and then just always put the bottom side back down. I print mainly ABS on that sheet and it doesn't seem to lose adhesion as easily as a smooth sheet printing PLA. |
|
Originally Posted By turtle2472: I looked at getting another AMS2 but they are out of stock now so I'm going to hold off. It was going to be that AND two power adapters. One of the other threads mentioned needing to have the external power supply to best use them. More questions: When does BBL ever actually have filament in stock? Every time I look at buying some they are out. With bulk buying they are about the same price as others on Amazon but they never seem to have stock. Plus, as silly as it is, I'd like to get the RFID chips from some of them to make loading filament into the AMS simpler. If it is there, I would like to be able to use it without having to manually program it. Second question is how often should I actually wash my build plate? I do not touch it, ever. I printed a PLA scraper and flex it using the edge tabs. Speaking of RFID, can I get a repo of someone reading the chips so I can just clone them onto NFC/RFID tags I got from Amazon? I'm thinking something like these I got a long time ago. I'm wondering if there is a repo out there that has the data from the BBL spool chips that I can clone onto the NFC chips. I've got a ton of them from home automation things I use them for. I've heard a few people say that it takes them a few months to recover from end of year sales, plus the influx of a bunch of new printer owners as a result.....but normally stock on things eventually levels out. I've only had a Bambu for a few months, so I have zero first hand knowledge. I typically by Bambu when I can, the RFID is a nice bonus.....when you only need 1 or 2 spools of something, don't forget to check Best Buy and other retailers that carry Bambu. I needed a couple spools of PETG that Bambu had been out of stock on for a while but Best Buy had them with free shippinig. No idea on programming other RFID chips. |
EP429: Today's lesson - Don't provoke ARFCOM. People will see your butthole.

|
Originally Posted By ScooterInVegas: Have you googled fan settings for 3D printing ABS? Your auxiliary fan should be off for ABS. And your part cooling fan should be off or at a very low speed and speed up a little while doing an overhang or bridging. Originally Posted By ScooterInVegas: Originally Posted By turtle2472: I thought it had active heat, but I guess it is just recirculation. Have you googled fan settings for 3D printing ABS? Your auxiliary fan should be off for ABS. And your part cooling fan should be off or at a very low speed and speed up a little while doing an overhang or bridging. A case where google isnt automatically your friend. When your chamber is enclosed with good heat fan can increase overhangs and strength of ABS. Lots of folks dont understand abs due to internet lore.. but its actually pretty easy to work with if enclosed and warm. I would suggest 0% if no overhangs up to 75% if you have tricky parts and overhangs. |
What causes spider webbing with PETG? I know moisture can, but My AMS is 9% and I dried it for 12 hours before printing with it.
|
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: What causes spider webbing with PETG? I know moisture can, but My AMS is 9% and I dried it for 12 hours before printing with it. https://turtle2472.com/ar15/IMG_1812.jpeg In my experience petg is just like that. |
|
Originally Posted By turtle2472: What causes spider webbing with PETG? I know moisture can, but My AMS is 9% and I dried it for 12 hours before printing with it. https://turtle2472.com/ar15/IMG_1812.jpeg Time for the flame treatment. Spider webbing disappears |
Tennessee Squire
|
Originally Posted By turtle2472: Thanks for sharing the video of it. I'm definitely not ready to cut a hole in the wall of my printer yet. I mean, it is just 3 weeks old right now. Give me two more and maybe! I did print with my PETG today and it is working out great. I just did default "Generic PETG" in my AMS and it is printing perfectly so far. My chamber is only 40°C with the bed being 70°C. I did this to my P2S, works great for printing cf nylons 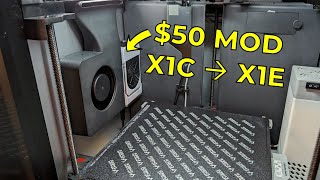 Bambulab X1C - $50 HEATED CHAMBER |
|
Originally Posted By turtle2472: What causes spider webbing with PETG? I know moisture can, but My AMS is 9% and I dried it for 12 hours before printing with it. https://turtle2472.com/ar15/IMG_1812.jpeg Keep in mind the AMS is telling you the moisture of the air, not the filament. I had a roll of PETG show up once that must have been stored underwater prior to shipping....it took 3 rounds of drying before it stopped causing me trouble. That might not be your issue here, just wanted to point out that the AMS can give you a false sense of how dry filament is. |
EP429: Today's lesson - Don't provoke ARFCOM. People will see your butthole.
|
Originally Posted By turtle2472: What causes spider webbing with PETG? I know moisture can, but My AMS is 9% and I dried it for 12 hours before printing with it. https://turtle2472.com/ar15/IMG_1812.jpeg Your filament is wet.  PETG can look like that. It can also print as clean as PLA. These are all PETG, and these filament profiles aren't even particularly well tuned. I had Polymaker PETG on my Prusas tuned exceptionally, no whisps at all, granted I was doing 70kg/mo so a good tune was worthwhile. Attached File Attached File Attached File |
|
So my filament is wet. I can work with that. I'll run that thing through my drying cycle a few times. Sadly, I can't print while it is happening since I only have the one AMS. Storage is dry now. I did manage to print off more spool desiccant holders so each spool has its own desiccant pack right now. I'll just run it through the AMS for a couple more runs. I also replaced the included desiccant packs with the AMS with a printed one and reusable Dry & Dry. It makes sense that my AMS is reporting the air RH and not the spool. Also makes sense that the spool isn't as dry as I would think in the middle where the heat is only barely getting to it in one run. After I finish the job that's running right now I'll start cooking my PETG again. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: So my filament is wet. I can work with that. I'll run that thing through my drying cycle a few times. Sadly, I can't print while it is happening since I only have the one AMS. Storage is dry now. I did manage to print off more spool desiccant holders so each spool has its own desiccant pack right now. I'll just run it through the AMS for a couple more runs. I also replaced the included desiccant packs with the AMS with a printed one and reusable Dry & Dry. It makes sense that my AMS is reporting the air RH and not the spool. Also makes sense that the spool isn't as dry as I would think in the middle where the heat is only barely getting to it in one run. After I finish the job that's running right now I'll start cooking my PETG again. This is how you end up with multiple AMS's / HT's and even an external dryer.....I've heard In all seriousness though, drying via the AMS2 is always going to have limitations / tradeoffs. Unless you only keep it loaded with 4 of the same filament type, your going to be limited by whatever the lowest temp spool is. If you have 3 spools of PLA and 1 spool of PETG, you wouldn't want to set the time / temp to dry the PETG, since it could mess up the PLA. On the H2D, they added dry while printing to the latest firmware but it automatically restricts it to a lower temp, so it doesn't dry out the filament in the tube. It's a great option but using it to dry is going to interrupt your printing at some point. Adding an HT to your current AMS, would let you dry at any temp in the HT while printing from the AMS but still give you the flexibility to also print from the HT. I've got a 2 spool standalone dryer that I bought before I had anything Bambu and even though I have a AMS2 and 2 HT's, it still gets some use. It's a vicious cycle, the more you print, the more spools you buy at a time, the more you need to dry.
|
EP429: Today's lesson - Don't provoke ARFCOM. People will see your butthole.
|
Yeah, that sounds about right. I just ordered another 4 spools of Sunlu white PETG since I'm really low on the one I got with my 10 spool bundle. Maybe the HT is my next thing to buy. That or the Pi x4 thing. ETA: Drying for 24 hours started since 12 wasn't enough. I figure I'll dry everything out of it and then keep it stored in the tubs with <15%RH. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: Yeah, that sounds about right. I just ordered another 4 spools of Sunlu white PETG since I'm really low on the one I got with my 10 spool bundle. Maybe the HT is my next thing to buy. That or the Pi x4 thing. ETA: Drying for 24 hours started since 12 wasn't enough. I figure I'll dry everything out of it and then keep it stored in the tubs with <15%RH. I went the P2S + AMS route, then got the HT (which is really helpful to have a second dryer that can go up to 80 degrees - you can also 'mod' it to dry while printing). But be aware that if you get into more engineering filaments, the HT will show it's limitations. There are other dryers that can go hotter, or even anneal, but IME they're not a replacement for a proper lab oven. |
|
Originally Posted By turtle2472: Yeah, that sounds about right. I just ordered another 4 spools of Sunlu white PETG since I'm really low on the one I got with my 10 spool bundle. Maybe the HT is my next thing to buy. That or the Pi x4 thing. ETA: Drying for 24 hours started since 12 wasn't enough. I figure I'll dry everything out of it and then keep it stored in the tubs with <15%RH. What temp is it actually getting to? Do you have the external power adapter? If not, you need it. It won't get hot enough to dry well. Personally I think even allowing it to be powered by the printer was a mistake. It shouldn't even be an option. Get the external adapter as it won't dry for crap without it. Run it at 65C for 24 hours just to be good and sure. I 3 found that my Sunlu S4 dries better than the AMS 2. At least my limited testing shows that the total air temp.ij the AMS doesn't reach as high as it claims vs the S4 actually does. Again just what I seen in my 2 AMS 2s and one S4. My HT seems to do a great job. |
|
Originally Posted By -Obsessed-:What temp is it actually getting to? Do you have the external power adapter? If not, you need it. It won't get hot enough to dry well. Personally I think even allowing it to be powered by the printer was a mistake. It shouldn't even be an option. Get the external adapter as it won't dry for crap without it. Run it at 65C for 24 hours just to be good and sure. I 3 found that my Sunlu S4 dries better than the AMS 2. At least my limited testing shows that the total air temp.ij the AMS doesn't reach as high as it claims vs the S4 actually does. Again just what I seen in my 2 AMS 2s and one S4. My HT seems to do a great job. It does get to 65°C but seems to hover between 60-65.  I'll order the power supply for it on my next Bambu order though so it won't be a problem. I was tempted to print a desiccant pack that has an insert for the rectangle hygrometers so I could slide one in that isn't from the internal sensors so I can compare, but I'll leave it as is for now and "trust" the internal readings. One step at a time. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: It does get to 65°C but seems to hover between 60-65. https://turtle2472.com/ar15/IMG_1817.jpeg I'll order the power supply for it on my next Bambu order though so it won't be a problem. I was tempted to print a desiccant pack that has an insert for the rectangle hygrometers so I could slide one in that isn't from the internal sensors so I can compare, but I'll leave it as is for now and "trust" the internal readings. One step at a time. Yeah I used a standard rectangle hygrometer and it was reading 50ish on the hygrometer temp, vs the 60ish the AMS was reading. With the power cable they are both reading 64-66. I had swapped my printers around and was having a hell of a time wondering why it wasn't drying well. I had left the AC adapter unplugged.  I left room for another HT that I'll get in the next 2 months or so. Attached File |
|
Originally Posted By -Obsessed-:Yeah I used a standard rectangle hygrometer and it was reading 50ish on the hygrometer temp, vs the 60ish the AMS was reading. With the power cable they are both reading 64-66. I had swapped my printers around and was having a hell of a time wondering why it wasn't drying well. I had left the AC adapter unplugged. I left room for another HT that I'll get in the next 2 months or so. https://www.ar15.com/media/mediaFiles/467079/12504_jpg-3723378.JPG Nice setup! So I guess I'll print that holder with the hygrometer slot in it after all. Well, in about 20 hours at least. Is the plug on the power adapter standard 5.5mmx2.5mm barrel? I can get a matched spec one from Amazon for $15. Not trying to be cheap, just don't want to pay shipping from Bambu and they don't have enough filament I want to build up a cart right now. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
 WooHoo! Total drying time of 36 hours and I have a clean print. Maybe the Sunlu took a trip under the seas instead of across them. ETA: Sad face.   Is this because I printed a PLA job selecting PETG from the phone? As in, I didn't do it through Studio so that it would use the PETG profile instead of PLA the original MW posting used? |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
| I love the fact that this printer looks before printing. I forgot to clear off the hygrometer holders before starting my next job. It yelled at me. It was better than just shoving the previous prints around and getting stuck. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”

|
Using Bambu studios, can you cut a part on 2 planes? For instance let's say you have a 35mm wide by 45mm tall by 108mm long block and you want to cut 10mm off the top. Making the part now 35mm tall. However you want to keep 15mm on one end the full height of 45mm I am trying to cut a M&p full size frame to a compact size but keep the short area the extends to be even with the magazine plate thickness and I am having a hard time figuring out if I can and if so how. Any help appreciated. |
C co 2/325th AIR 91-96 11B1P
Father of 6 un-socialized homeschoolers and grandfather to 2 awesome little boys and the most beautiful granddaughter in the world.
Father of 6 un-socialized homeschoolers and grandfather to 2 awesome little boys and the most beautiful granddaughter in the world.
|
Have you tried turning the temperature down 5° and increasing the retraction rate by .5 mm? I would try that first and maybe bump the retraction speed up a little bit after a test print. |
|
Originally Posted By ScooterInVegas:Have you tried turning the temperature down 5° and increasing the retraction rate by .5 mm? I would try that first and maybe bump the retraction speed up a little bit after a test print. I've not made any changes to any default settings. Partially because I have no clue what I'm doing and every failure/imperfection leads me down a rabbit hole to figure out. The rest is because I'm spoiled by Bambu Handy and most of my jobs are from scrolling MakerWorld and hitting print. I really don't know what I'm doing. I was thrilled when I was able to take a cylinder in Bambu Studio and adjust the sizing so it was 2.5" x .75" from whatever smaller size it was!I think part of what I'm seeing is that my printer just sees the Sunlu Filament as "Generic PETG" rather than Sunlu. In Studio, I go to the prepare section and I see Sunlu in the filament sector, but it is greyed out and "Unsupported" even though it is what I have. I feel like I'm going to have to figure out the Custom section and just create custom profiles in Studio for them even though they should be systemwide now.  I'm scratching my head on this one. I know so little and still connecting dots. ETA: I went through and removed all the other BBL printer models from my Studio and Sunlu is no longer an option. Seems it was tied to one of the other model printers. So a custom filament is my only way to add it now. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Please do! I'm picking up a ton along the way but there are so many little things once you start straying away from BBL specifics. If they had their PETG in stock I would have likely just bought it instead of Sunlu. Thing is, that is REALLY limiting compared to the amount of materials out there. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: Please do! I'm picking up a ton along the way but there are so many little things once you start straying away from BBL specifics. If they had their PETG in stock I would have likely just bought it instead of Sunlu. Thing is, that is REALLY limiting compared to the amount of materials out there. It's not hard to fully calibrate a filament but it does take time. Time that most don't want to mess with. But the truth is as speed increases, proper calibration becomes MUCH more important. I'll try to get something together over the next week or so. FWIW, Sunlu filament actually prints exceptionally well for it's price. It's a bit more oozy than Polymaker, Prusa, or Bambu, but it's consistent filament and is a third the price. 8.25/roll on sale is hard to beat. It is WAY more sensitive to being wet than others IME. I try mine for 24 hours at 65C in my S4. Also, one of the reasons I'm also a proponent of dry boxes is that repeated drying can degrade filament. PLA can only handle about 40 hours of total dry time before it degrades into a brittle mess and k factor starts to creep up. PETG gets 40-60 hours before it starts to degrade and it starts to string more. I haven't researched other filament types so I don't know their drying cycle tolerance, but I presume most are sensitive to some extent. |
I'm willing to make the tweaks and work through it if it will work as I expect it would. I get that something I print won't have the polish of something that is injection molded or other such manufacturing methods, but this is just ugly and I don't care because it is going to sit in my AMS so I can see at a glance what it really is in there while holding a little desiccant. Sunlu custom PETG profile on left replacing the Generic PETG profile print on the right. I just printed the one on the left because the cap on the style on the right wedged between the feeders and I didn't want them having any pressure on them. The one on the left is staying even though it looks like crap. |
Louis L'Amour, “To make democracy work, we must be a nation of participants, not simply observers. One who does not vote has no right to complain.”
|
Originally Posted By turtle2472: I'm willing to make the tweaks and work through it if it will work as I expect it would. I get that something I print won't have the polish of something that is injection molded or other such manufacturing methods, but this is just ugly and I don't care because it is going to sit in my AMS so I can see at a glance what it really is in there while holding a little desiccant. https://turtle2472.com/ar15/IMG_1834.jpeg Sunlu custom PETG profile on left replacing the Generic PETG profile print on the right. I just printed the one on the left because the cap on the style on the right wedged between the feeders and I didn't want them having any pressure on them. The one on the left is staying even though it looks like crap. Wet filament left, dry filament on right. EXACT same roll. EXACT same gcode. Attached File |